Load data
Carrier spacing and capacity defined by part weight and geometry.
Overhead conveyor systems, manual monorails and Power & Free conveyors move parts through surface preparation, painting and curing with controlled process times.
Request a project proposal ↗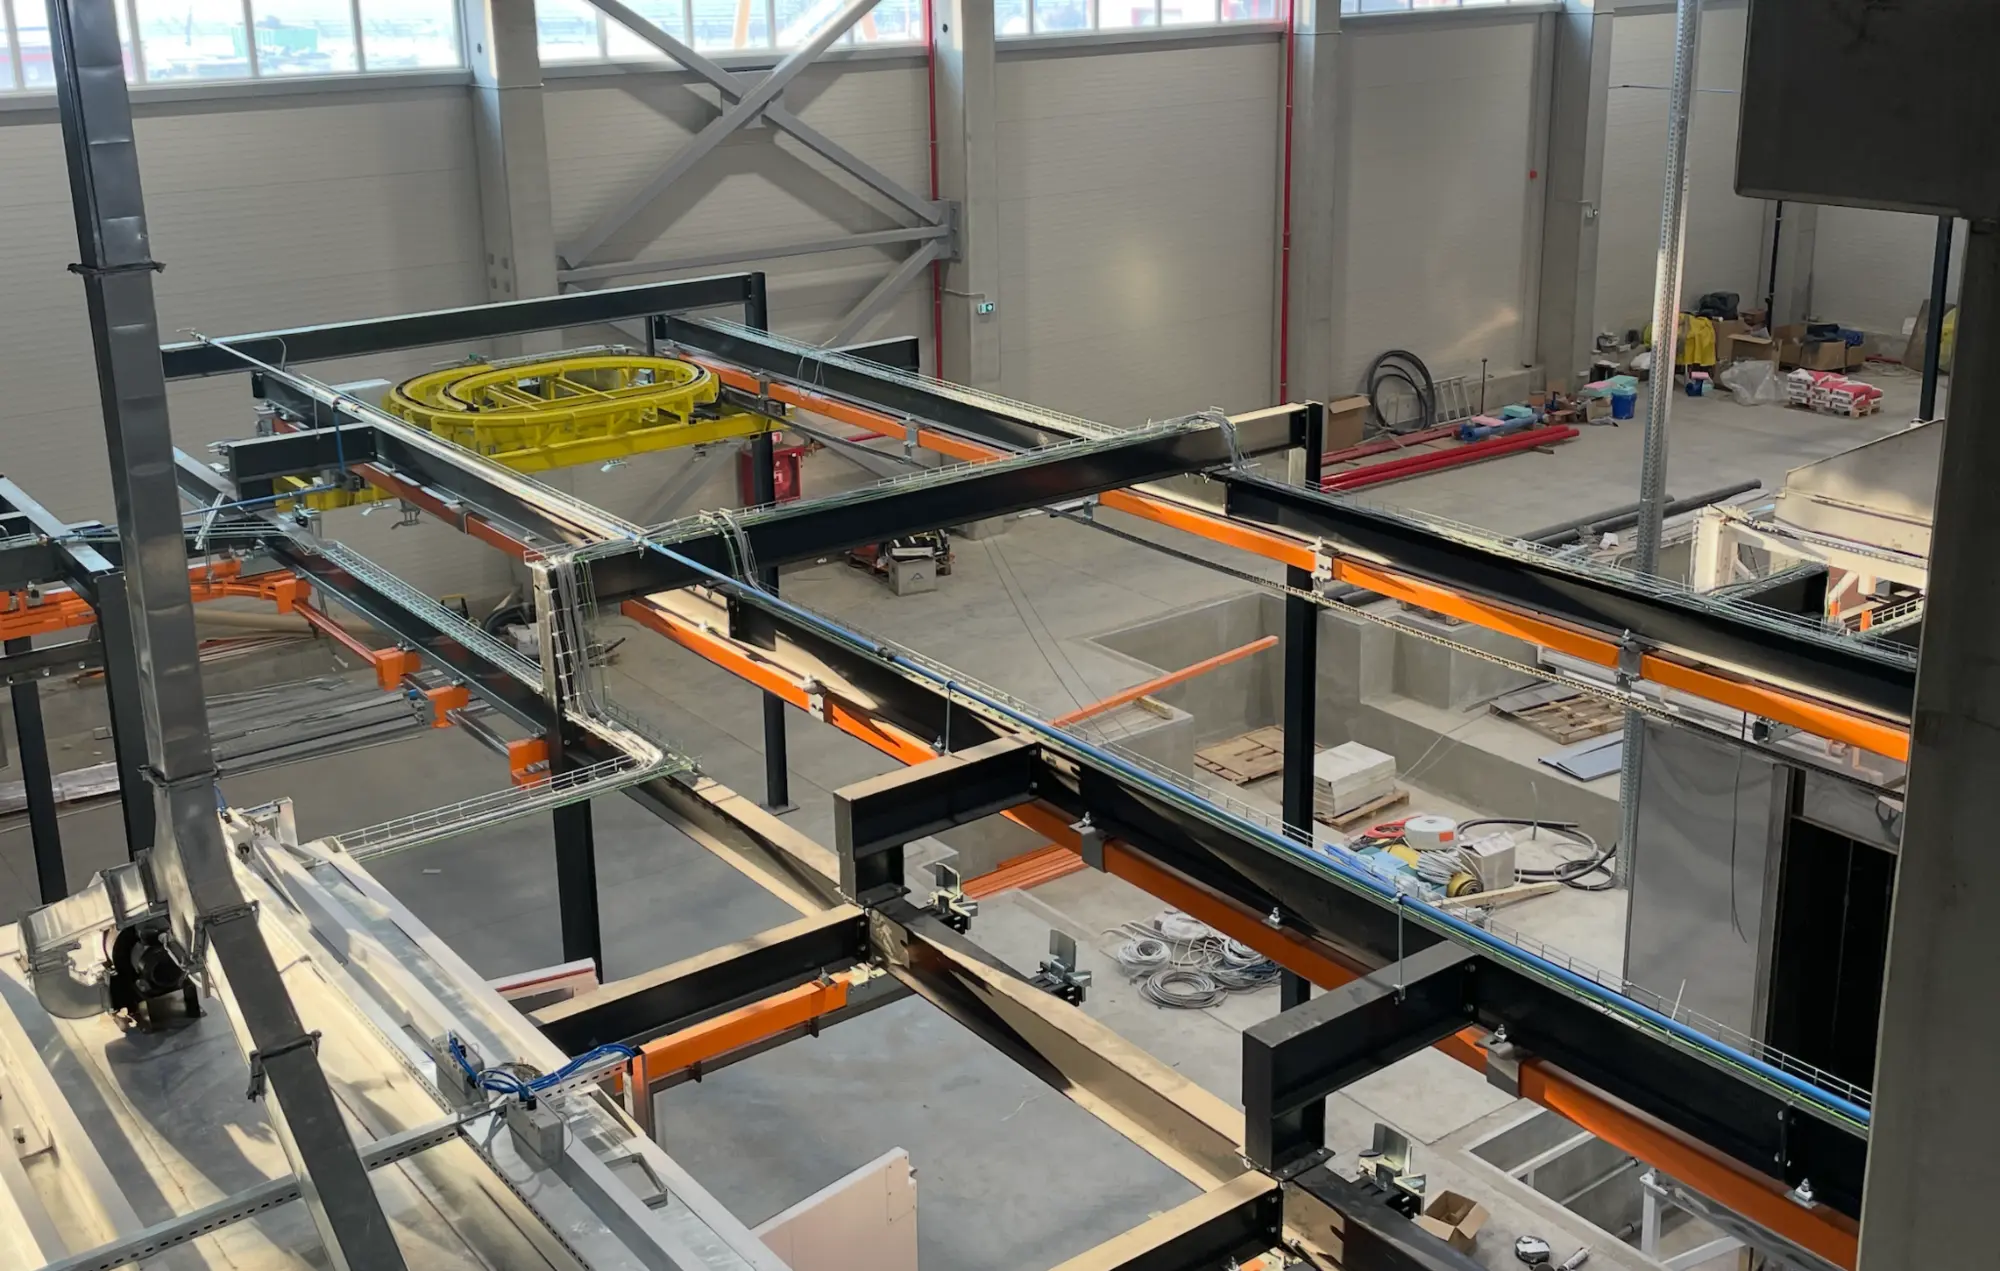
Engineered for your process
Part dimensions, hanging method, load weight, takt time and process sequence determine the correct conveyor architecture.
We integrate manual monorail, continuous overhead and power-and-free systems with pretreatment, booths, ovens, cooling and loading zones.
A Power & Free conveyor, often abbreviated P&F conveyor, allows workpieces to stop or accumulate independently where the layout requires it. Conveyor selection starts with hanging weight, carrier spacing, route and the dwell time at each finishing stage.
Carrier spacing and capacity defined by part weight and geometry.
Continuous, indexed or independently routed trolley movement.
Interfaces coordinated with every process enclosure and control panel.
Related systems
System planning
A manually moved system can suit flexible batch work where operators control movement between stages.
Conveyor choice depends on load, route, process times and whether workpieces need to stop or accumulate independently.
Provide maximum part dimensions, hanging weight, loading method and required output per shift.
Related installation
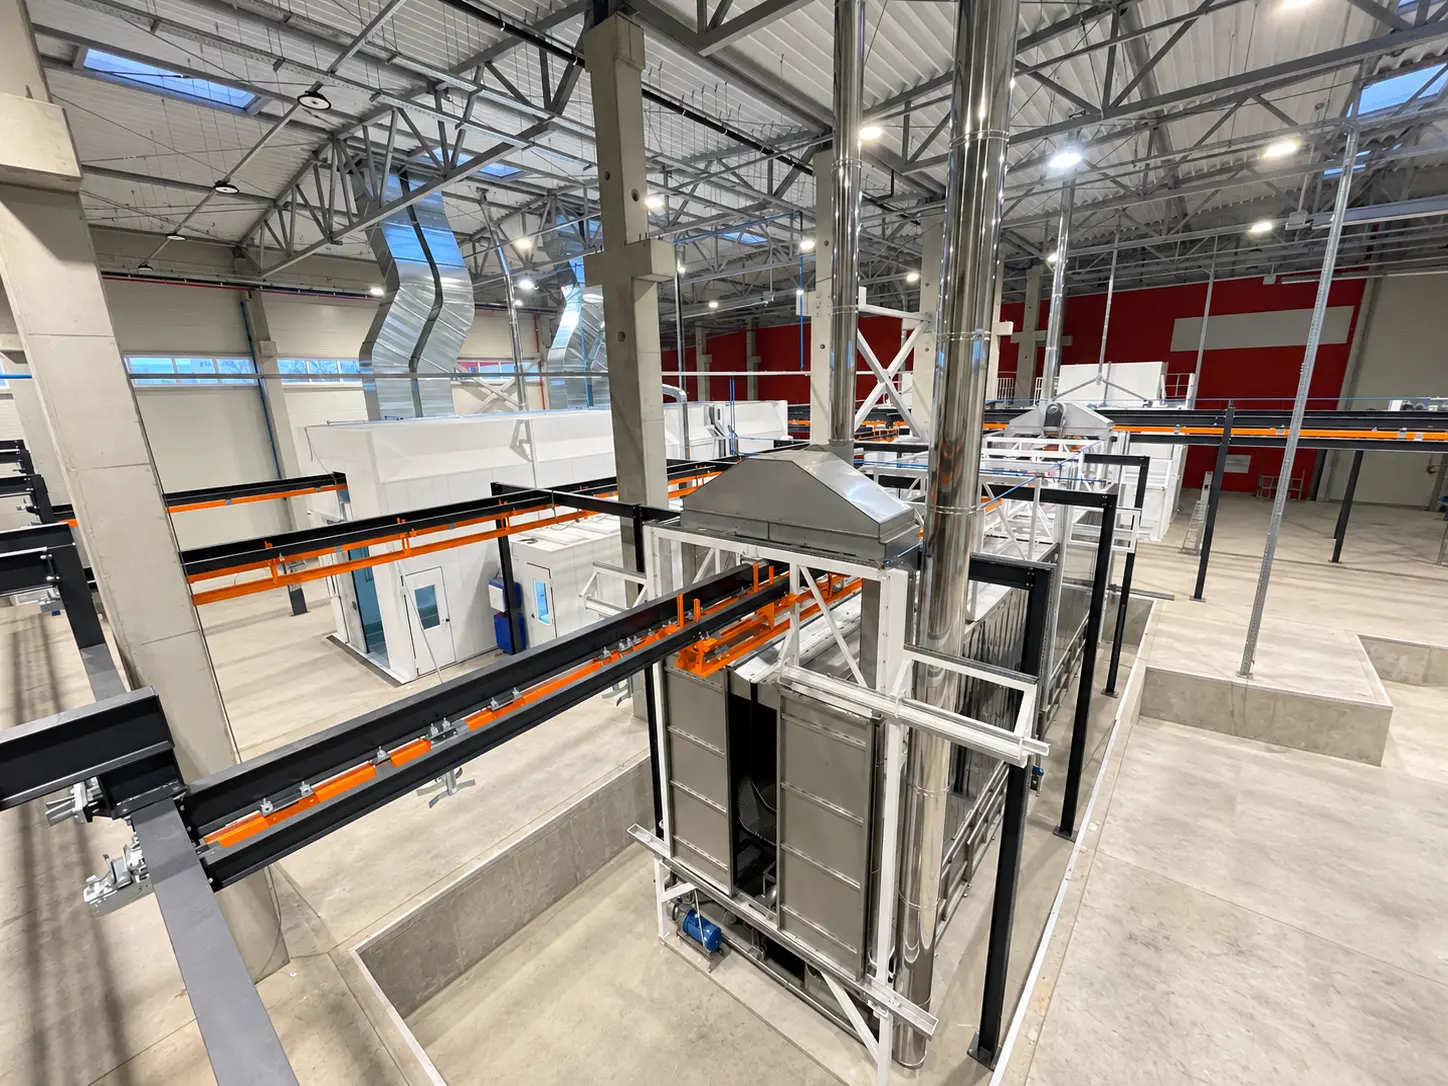
Explore the installed system, its configuration and project photographs.
View project ↗